
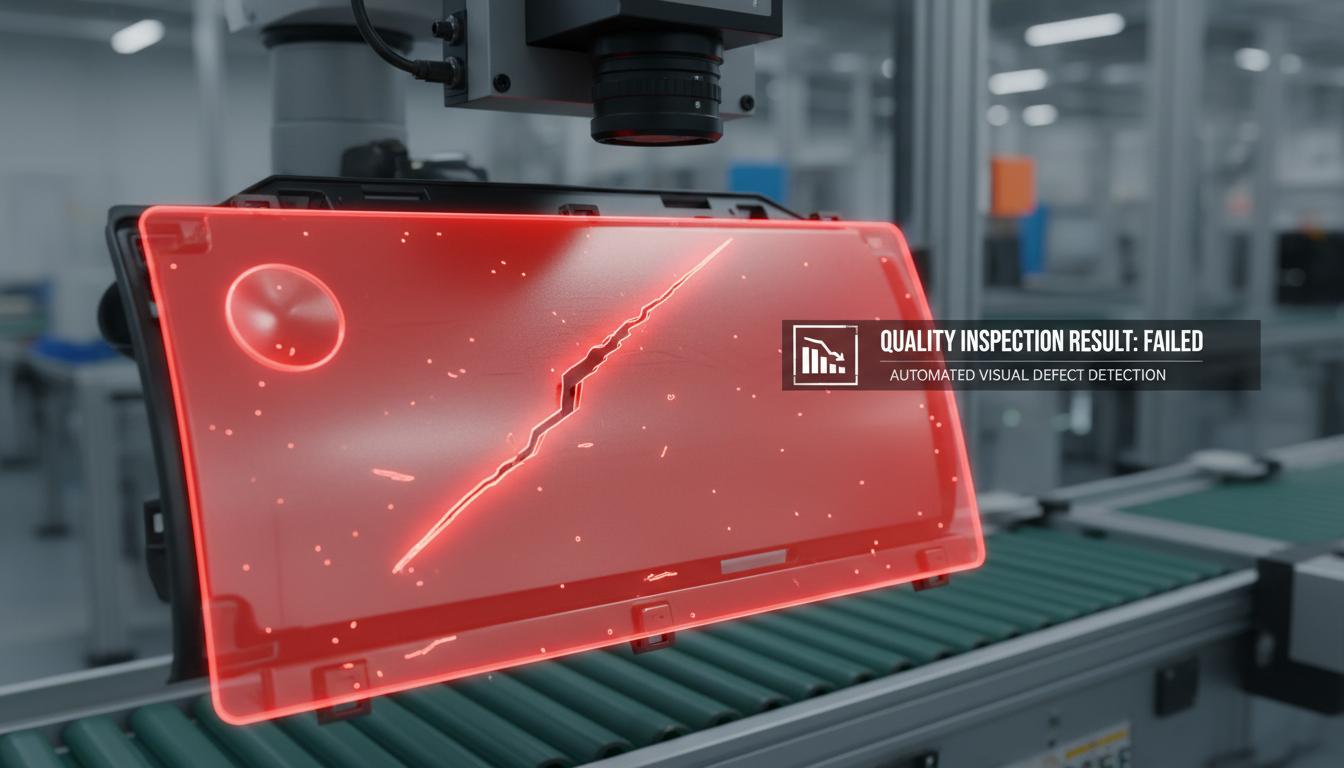
Principles, Scenarios and Suitability
Surface inspection depends on differences in reflected light, colour or texture. Design lighting that reveals the target defect before choosing a model. Acceptable marks must be defined by product requirements; not every difference from a reference image is a defect.
A shiny surface resembles a mirror: changing the light angle changes what appears. Scratches in one direction may become clear while others disappear; adding a model alone cannot solve this. A defect violates requirements, whereas finish is the intended surface condition, such as matt polishing or coating. Reviewers must agree which marks affect function or appearance and which are normal manufacturing variations.
A bounding box gives an approximate location; a mask describes the marked area in detail. Measuring size requires scale calibration and an edge definition consistent with acceptance criteria. More angles and lights improve coverage but add time and image-matching work. Trial marks in several directions with reviewers before choosing a method. Hold ambiguous marks rather than rejecting every difference and creating excessive manual inspection.
Scroll the diagram horizontally to inspect all details.
Illustrative Design Scenario
Illustrative design scenario: oblique lighting reveals scratches on metal, while reviewers distinguish scratches from removable dust. Multiple views expose marks in different directions, but their results must be associated with the same item before a decision is made.
Suppose one line disappears after cleaning by an authorised procedure, while another remains. This gives reviewers evidence distinguishing residue from a permanent mark. Pixel intensity is not a direct measure of scratch depth. If depth determines acceptance, add an appropriate measurement method and retain human decisions as a traceable reference.
Operators might choose diffuse light to reduce shadows or oblique light to emphasise shallow scratches, but they suit different marks. Trial reference items from multiple batches and borderline acceptable marks without altering saleable products to create defects. A future multiple-camera design must verify that each side belongs to the same item before combining results. Image count must not inflate item count.
Inputs and Prerequisites
Prepare surface types, minimum defect sizes, severity criteria, images from multiple batches, and lighting and lens plans. Include acceptable marks so training does not encourage rejecting every visible variation.
Record material, coating, light angle and capture distance with images. Labels should identify a reviewer and reasoning. Do not force disputed marks into good or bad classes merely to fill the dataset faster.
Results should identify mark type, location, visible angle and the surface area completely inspected. A high score expresses model confidence for its trained task, not physical severity or component strength. Separately identify areas near edges or holes that light cannot reach. A whole-surface conclusion requires reviewer confirmation of view coverage; more images alone do not extend the inspected area.
Trial and Integration Workflow
- 1Trial lighting and capture distance until target defects are clearly visible.
- 2Have reviewers annotate masks or boxes according to agreed defect definitions.
- 3Split by batch and assess how multiple views are combined per item.
Evaluation and Acceptance Criteria
Report recall for important defects and false rejects per item, broken down by size, location and surface type. Calibrate image units when measuring scratch length. Acceptance should include edge defects and images with strong reflections.
Recall is the proportion of actual defects detected. Report sample counts too, because a small number of rare marks supports only limited conclusions. Split by batch so repeated images of one item cannot cross between training and testing.
Have reviewers sample passed surfaces and review flagged ones. Separate lighting problems from acceptance-definition problems before adjusting the model. Check lengths against a reference instrument if size determines acceptance; camera resolution alone cannot convert pixels into valid physical measurements.
Scroll the diagram horizontally to inspect all details.
Failure Cases and Limitations
Oil, dust and changed surface finishes may resemble defects, while subsurface marks are invisible. Results on one surface type must not be presented as evidence of suitability for every material without further testing.
Changing material suppliers may change normal colours and patterns. Review real samples before adding them to the reference set. Do not conclude that quality has declined or teach immediate acceptance without an authorised reviewer.
Surface inspection screens only the visible scope; it does not replace internal inspection or certify products. Extending defect types and materials is a new study requiring checks of lighting, criteria and test results, not an already installed capability.
Practical Checklist
- Does the lighting reveal defects in every relevant direction?
- Do reviewers agree on examples at the good/bad boundary?
- Are multiple views prevented from counting as multiple items?